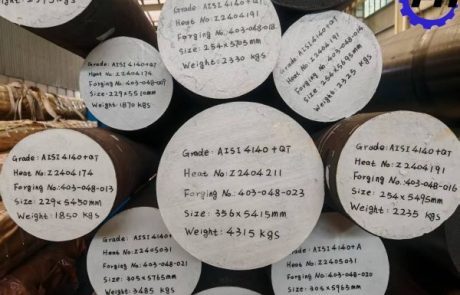

4140 (USA), 42CrMo4 (Europe), and SCM440 (Japan) all refer to low-alloy steels with a carbon content of approximately 0.40%, a chromium content of approximately 1.0%, and a molybdenum content of approximately 0.2%.They have a tensile strength of 900–1200 MPa in the quenched and tempered (Q&T) state and exhibit good fatigue resistance, impact toughness, and overall hardening ability at medium cross-sectional dimensions.
They are functionally interchangeable in most engineering applications, so the practical question is rarely “which is better?”, but rather “which product meets the customer’s required certification standards?”
This article analyzes and lists the differences in composition and mechanical properties, explaining in what ways these differences are crucial.
International Standards & Equivalent Grades
Each grade originates from a different national standards system, but all three are recognized as international equivalents by steel producers, classification societies, and engineering handbooks worldwide.
| Grade | Standard | Steel Family | Primary Region |
| AISI 4140 | ASTM A29 | 41xx Cr-Mo | United States |
| 42CrMo4 | EN 10083-3 | Cr-Mo quenched & tempered | Europe / Germany |
| SCM440 | JIS G4053 | Cr-Mo machine structural | Japan |
The Chinese national grade 42CrMo (GB/T 3077) is also a near-equivalent, with a slightly narrower Mn range (0.50–0.80%) and Mo capped at 0.25%. It is frequently substituted in Asian supply chains but is not analyzed in detail here.
Chemical Composition Comparison
Composition is the most obvious difference between these three standards, although they overlap considerably in practical applications. The table below lists the elemental standard ranges for each steel grade.
| Elements (%) | 4140 | 42CrMo4 | SCM440 |
| Carbon (C) | 0.38-0.43 | 0.38-0.45 | 0.38-0.43 |
| Chromium (Cr) | 0.8-1.1 | 0.9-1.2 | 0.9-1.2 |
| Molybdenum (Mo) | 0.15-0.25 | 0.15-0.3 | 0.15-0.3 |
| Manganese (Mn) | 0.75-1.0 | 0.6-0.9 | 0.6-0.9 |
| Silicon (Si) | 0.15-0.35 | 0.1-0.4 | 0.15-0.35 |
| Phosphorus (P) | ≤0.035 | ≤0.025 | ≤0.03 |
| Sulfur (S) | ≤0.04 | ≤0.035 | ≤0.03 |
What do the composition differences actually mean?
First, 4140 steel has a relatively high lower limit for manganese content (0.75% vs. 0.60%), which gives it a certain advantage in hardenability in the low content range, but its overlapping area (0.75%–0.9%) usually covers the other two.
Secondly, 42CrMo4 and SCM440 raise the lower limit of chromium content to 0.90% (0.80% for 4140) and the upper limit of molybdenum content to 0.30% (0.25% for 4140). This slightly widens the hardenability range, meaning that the overall hardenability is more uniform in sections close to the upper limit of the steel grade’s properties.
The most important difference lies in phosphorus and sulfur. The maximum phosphorus content for 42CrMo4 is 0.025%, stricter than the 0.035% for 4140, meaning a significantly longer service life. Furthermore, the higher maximum sulfur content (0.040% for 4140) can improve machinability but reduces transverse ductility and fatigue strength. European and Japanese standards tend to lower sulfur content to improve purity.
Comparison:Mechanical Properties-Quenched & Tempered
| Properties | 4140 | 42CrMo4 | SCM440 |
| Tensile strength (MPa) | 850-1000 | 900-1100 | 850-1000 |
| Yield strength (MPa) | 650-800 | 700-900 | 650-800 |
| Elongation (%) | 12-15 | 12-14 | 12-15 |
| Impact toughness (J) | 30-50 | 30-45 | 30-50 |
| Hardness (HRC) | 28-32 | 28-32 | 28-32 |
| Hardenability (Jominy value) | Medium (lower Cr/Mo) | High (higher Cr/Mo) | High (higher Cr/Mo) |
Reading the property table above, when tested under the same conditions, the performance indicators of these three types of steel are not significantly different.
However, it should be noted that 42CrMo4 has relatively high strength due to its high chromium and molybdenum content. Additionally, the impurity content of SCM440 is strictly controlled, resulting in slightly better impact toughness than the other two.
Comparison:Heat Treatment Processes
| Process | 4140 | 42CrMo4 | SCM440 |
| Annealing | 830-850℃ | 830-850℃ | 830-850℃ |
| Normalizing | 850-900℃ | 850-900℃ | 850-900℃ |
| Quenching | 850–880℃/oil | 850–880℃/oil | 850–880℃/oil |
| Tempering | 500–650℃ | 500–650℃ | 500–650℃ |
| Hardening depth | Medium (≤50mm) | High (≤80mm) | High (≤80mm) |
All three grades of steel use the same heat treatment process, so no adjustments are needed for different grades.
All three grades are classified as “oil-hardening” with moderate through-hardening capability.It’s worth noting that the higher lower limit of chromium content (0.90% vs. 0.80%) and wider range of molybdenum content in 42CrMo4 and SCM440 give them a certain advantage in hardenability. However, in most cases, their compositions may fall within the overlapping range, resulting in minimal differences.
Comparison:Machinability & Welding Performance
Machinability
All three steel grades are considered “moderately machinable” in the annealed state (hardness approximately 180–229 HB), but “difficult to machinable” in the quenched and tempered state (hardness > 30 HRC).
Relative machinability rating (based on 1212 free-cutting steel = 100%):
- Annealed state: Approximately 55–65% for all three steel grades
- Quenched and tempered state (hardness 28–32 HRC): Approximately 40–50%
- Quenched and tempered state (hardness > 45 HRC): Requires cubic boron nitride (CBN) or ceramic cutting tools
Weldability
All three steel grades are difficult to weld. Their IIW carbon equivalents (CE = C + Mn/6 + (Cr+Mo+V)/5 + (Ni+Cu)/15) are all approximately 0.72–0.80, belonging to the “high hardenability – preheating required” category.
All three can follow the same welding procedure. Preheating temperature of 200–300 °C, low-hydrogen welding materials, and post-weld heat treatment are all required during welding.
Applications & Industry Use
All three grades are suitable for the same application areas: medium- to high-strength components that require a balance of strength, toughness, fatigue resistance, and wear resistance. Typical applications are listed below by industry.
- Automotive:Crankshafts, connecting rods, axle shafts, steering knuckles, transmission gears, constant-velocity joints
- Oil & Gas:Drill collars, tool joints, kelly bars, couplings, high-pressure tubing, downhole tools, subsea fasteners
- Aerospace & Defense:Landing gear components, actuator rods, armored vehicle drivetrain parts, weapon components
- Heavy Machinery:Gear shafts, spindles, pinions, sprockets, rams, press components, turbine shafts
- Fasteners:High-strength bolts, studs, nuts (Property Class 10.9, 12.9), threaded rods
- Tooling & Dies:Fixture components, jigs, mold bases, drill jigs, arbors, collets
4140,42CrMo4,SCM440:When Substitution is Safe?
Substitution is not automatic. Even if these grades are metallurgically equivalent, relevant documentation is required for substitution on certified drawings.Before substitution, it is essential to confirm with the customer or design authority and retain the material testing certificate (MTC EN 10204 3.1) for traceability.
Direct substitution between any two of these grades is safe when all of the following conditions are met:
1. The drawing or specification should specify “or equivalent material,” such as “4140 / 42CrMo4 / SCM440 or equivalent material conforming to ASTM A29 / EN 10083-3 / JIS G4053.”
2. The cross-sectional dimensions of integrally hardened parts should be ≤50 mm. For dimensions exceeding this, end-quench (Jominy) testing is required to verify hardenability.
3. The heat treatment process remains constant. The same austenitizing temperature, quenching medium, and tempering cycle are used. Cycles should not be “optimized” for alternative grades without re-verification.
4. Mechanical property requirements are within the overlapping area. Tensile strength 900–1200 MPa, yield strength ≥750 MPa, elongation ≥12%, hardness 250–340 HB. All three grades easily meet this range.
5. No special low-temperature impact requirements below -40 °C. If Charpy V-notch impact testing is specified at -40 °C or lower, 42CrMo4 steel with stricter P-value restrictions is preferred; actual test data are required to verify whether the alternative steel meets the requirements.
6. No NACE MR0175 / ISO 15156 acidic environment requirements. Acidic environments impose higher limits on hardness (≤ 22 HRC) and higher requirements on sulfur content. Low-sulfur steel grades should be used in acidic environments.
When choosing, it is necessary to comprehensively consider the part size, mechanical requirements, processing conditions and regional standards, and verify key performance through experiments when necessary.
Related 4140 Steel Products By Fuhong Steel
3000+ tons Inventory For 4140 Hot Rolled Round Steel Bar
SAE 4140 Steel Bar | AISI 4140 Alloy Steel-ASTM A29
One-Stop Solution For 4140 Steel Bright Bar
SCM440 | SCM430 Alloy Steel-JIS G4105

EN 42CrMo4 Steel |42CrMoS4| DIN1.7225